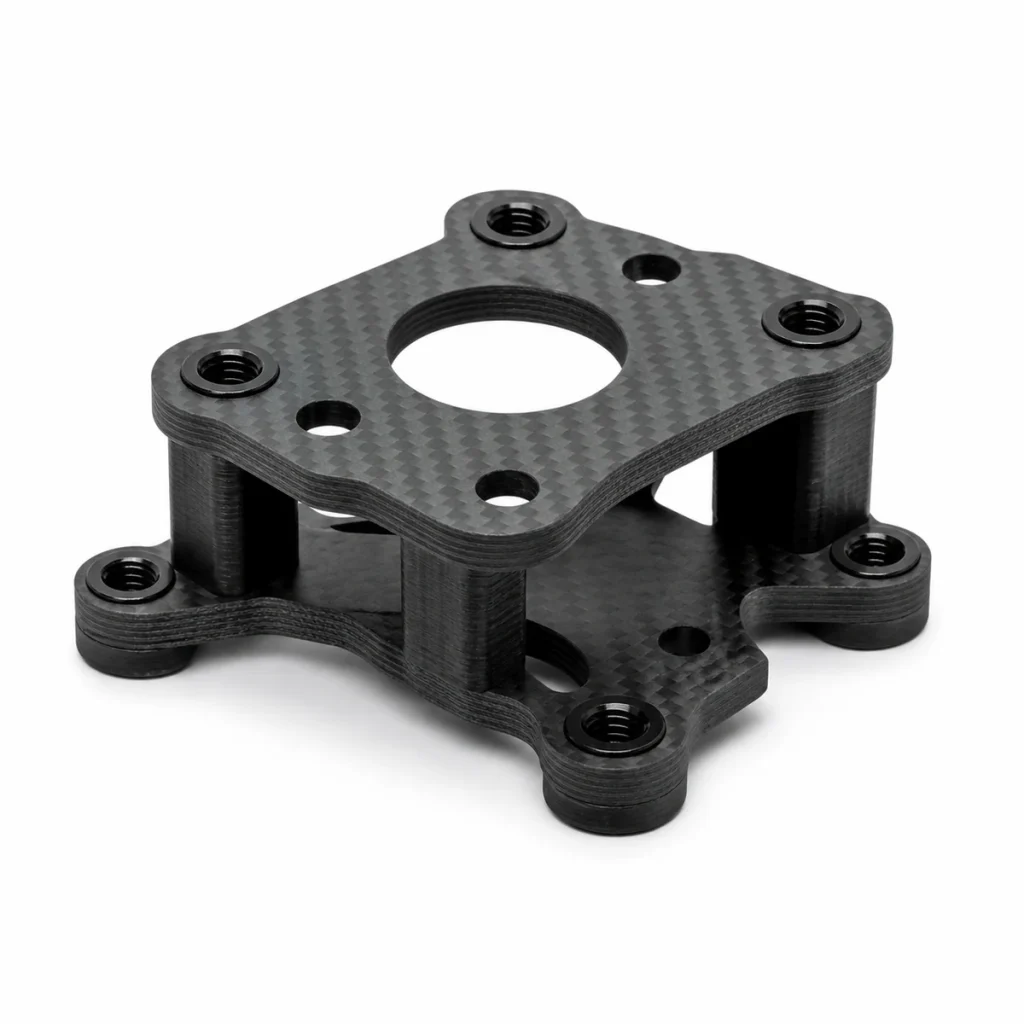
Decide on thread inserts in aluminum CNC parts before the threaded hole and surrounding boss are finalized. An insert can be considered when the joint needs a reinforced or repairable thread, repeated assembly or another defined performance requirement. It is a fastening system with its own hole preparation and installation requirements, not an accessory that can always be added to a finished hole. Select the actual insert product, review parent-material geometry and agree installation and inspection. If a direct aluminum thread already satisfies the design, an insert should not be added without a reason. The objective is an accepted joint, with the material, fastener and insert working together.
A clear quotation identifies whether inserts are supplied, installed and verified, rather than leaving those responsibilities between buyer and manufacturer.
State the problem the insert must solve
Record the fastener size, assembly frequency, expected loads and relevant service conditions. Identify whether the need is new-design reinforcement, repair, maintenance or a particular locking function.
Böllhoff's HELICOIL information describes wire inserts for thread reinforcement and repair in metals, including lower-shear-strength parent materials. Its product claims apply to the selected system and installation, rather than every product called an insert.
Do not use a metal-insert product description as evidence for an unrelated plastic installation. Material and installation method are part of the decision.
Select the system before defining preparation
Different insert systems require different preparation. Specify the product or an approved equivalent defined by appropriate requirements, then use its manufacturer's installation information.
| Item | What to specify |
|---|---|
| Insert identity | System, size, length and product variant |
| Parent material | Aluminum grade and relevant condition |
| Preparation | Required hole and thread geometry |
| Position | Installation depth and orientation where relevant |
| Final assembly | Mating fastener and locking requirements |
| Verification | Agreed installation and thread acceptance |
For aluminum CNC machining, provide the insert requirement with the initial drawing. It can affect boss size, available depth and access.
Avoid specifying a generic tap size while separately naming an insert whose preparation differs. The controlled documents should describe one coherent system.
Review material around the hole
An insert does not remove the need to design the parent part. Review edge distance, boss geometry, available bottom depth and neighboring features with the insert supplier's requirements.
Ask how installation access will be provided and whether another feature obstructs the tool. A hole that can be machined may still be awkward to install or inspect after surrounding work is complete.
The mating joint also needs review. Clamp load, fastener engagement and the load path should be approved by the responsible designer rather than inferred from an insert catalog picture.
If the proposal changes the aluminum geometry, record the approved change before machining.
Coordinate tapping, finishing and installation
Sandvik's tapping guidance explains the importance of material, prepared hole and chip evacuation in a tapping operation. Apply that manufacturing discipline to the insert's specified preparation rather than treating it as an ordinary unqualified thread.
Agree when finishing occurs relative to installation. The selected system, coating and functional requirements should determine whether additional masking, cleaning or verification is needed.
During custom CNC planning, clarify who supplies the inserts, who installs them and what is included in the quoted delivery. A machined insert hole and a completed installed insert are different deliverables.
Agree what the inspection proves
A visually present insert does not by itself demonstrate the required installation. Establish the checks appropriate to the selected system and the project's risk.
The agreed record might identify insert product, installed position, functional thread verification and any application-specific check. Do not request an arbitrary destructive test without defining its purpose and acceptance.
Use this release sequence:
- Approve the fastening system and parent geometry.
- Freeze manufacturer-specific preparation requirements.
- Coordinate finish and installation sequence.
- Define responsibility for components and installation.
- Agree final inspection and documentation.
- Record any permitted alternative or repair procedure.
For a repaired component, keep the repair approval explicit. A repair instruction should not quietly become the production drawing for future parts.
Questions about aluminum inserts
Does every aluminum thread need an insert?
No. Use the joint requirements to decide whether direct threads or an insert system is appropriate.
Can an insert be added after all machining is finished?
Sometimes, but preparation, surrounding material, access and finish need review. Plan it early.
Are all inserts of the same nominal size interchangeable?
No. Product geometry, preparation, installation and functional requirements can differ.
Can the shop choose the insert length?
It may recommend an option, but the design authority should approve the engagement and joint requirements.
Should the quotation include installation evidence?
State the required checks and records before ordering so the delivered scope is clear.
Related guides: Blind Tapped Holes: Separate Full Thread Depth from Drill Depth; CNC wall thickness guidelines for milled parts by material and height.
Include the selected insert in the package
Upload the aluminum drawing with insert specification, fastener details, material, quantity and finish. Ask YXT to review preparation, access, installation sequence and acceptance before production is confirmed.