
Wire EDM Machining
Services
Conductive materials from common steels to titanium and copper alloys
Factory-direct project review
Feature tolerances reviewed to the drawing
Prototype and production support
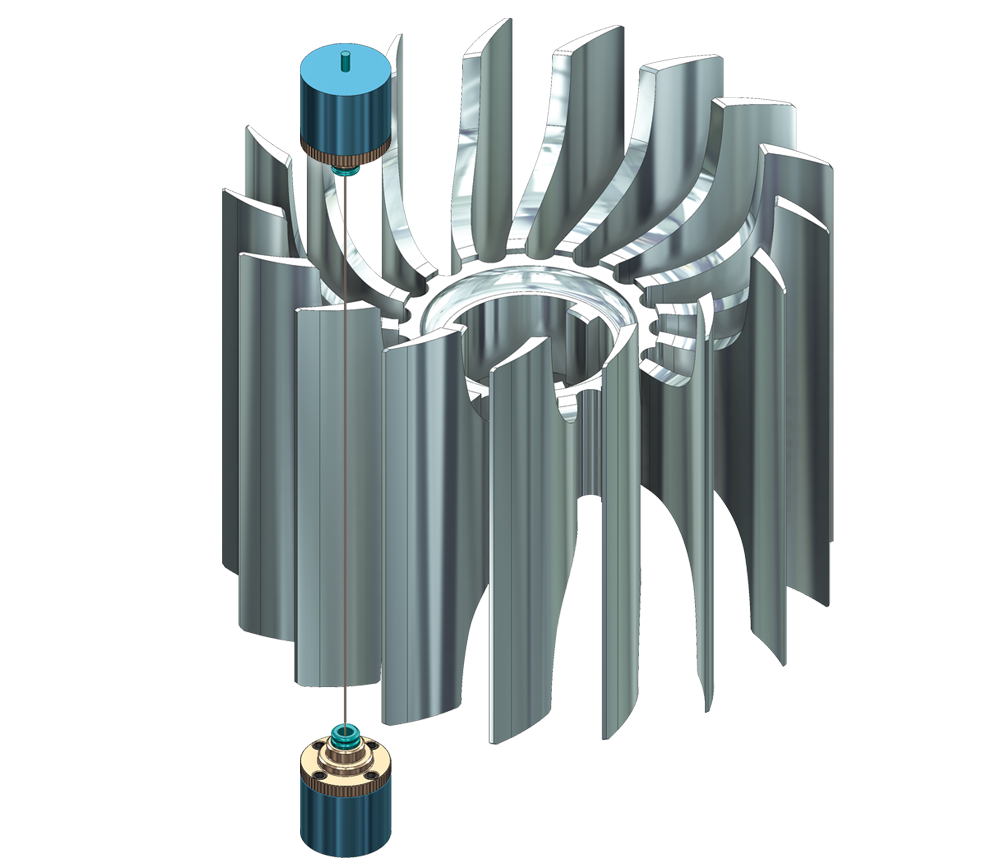
Your Custom Wire EDM Machining Preferred Supplier
YXT specializes in precision wire electrical discharge machining, serving customers who require complex, high-tolerance parts.
Our expertise in wire EDM enables us to efficiently machine delicate geometries, holes, and finishes in hard or exotic alloys that are difficult with conventional methods.
With over 15 years focused on advancing wire EDM, we routinely hold extremely tight tolerances down to +/-0.001″.
YXT leverages the latest wire EDM technology to deliver quality small-scale prototypes or high-volume production runs tailored to your application’s material and tolerance needs.
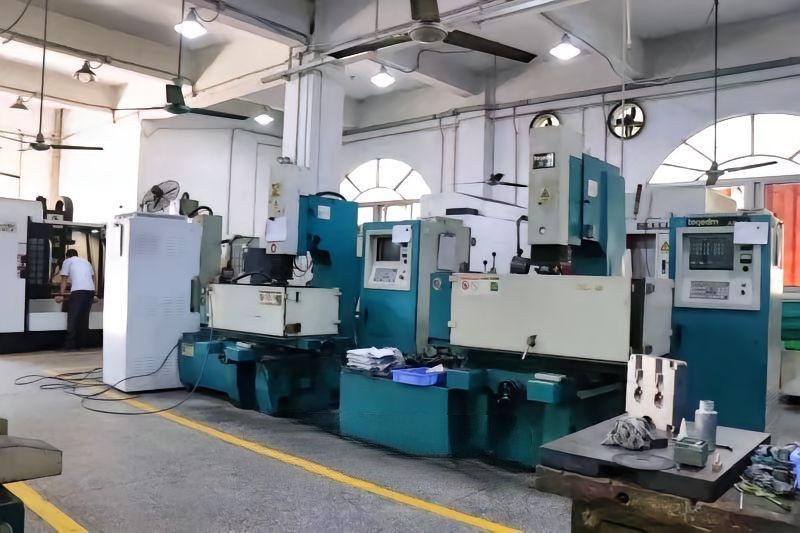
What is Wire EDM Machining
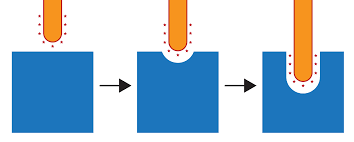
Wire electrical discharge machining (EDM) uses an electrically charged thin wire to cut and shape conductive materials with high precision.
The wire follows a programmed path through the workpiece, creating a narrow kerf while controlled electrical sparks remove material.
Because the process is non-contact, wire EDM is well suited to delicate profiles, hardened materials, small slots, and complex features that require tight dimensional control.
Types of EDM Machining
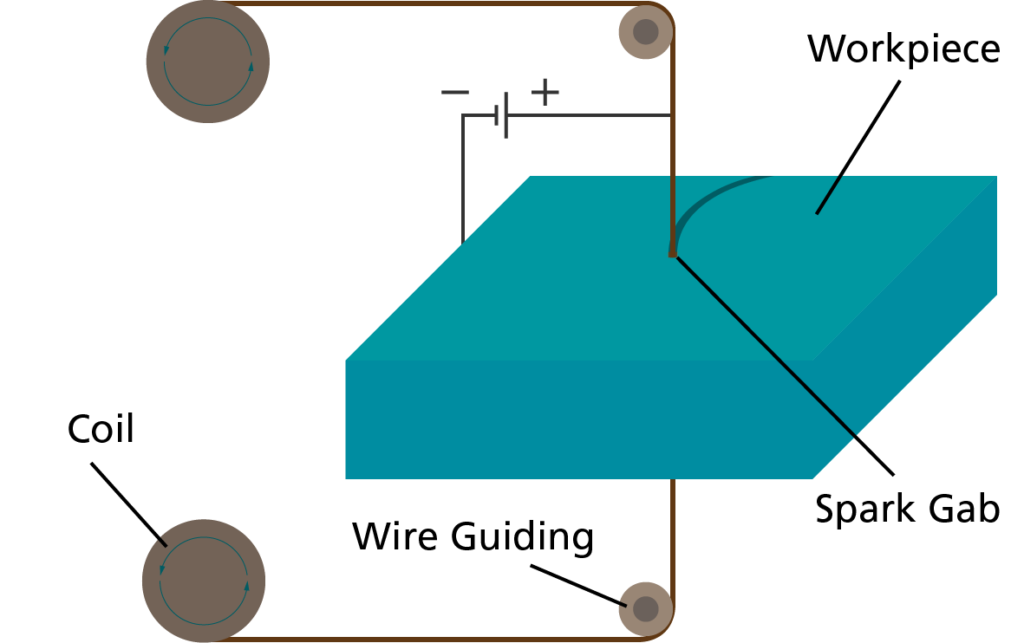
Wire EDM (Wire EDM Cutting)
Wire EDM operates using a continuously fed, thin wire electrode that slices through hardened metals to craft contours or cavities. The process is largely computer-controlled, ensuring precision and accuracy in intricate shapes.
The wire, commonly made of brass or stratified copper, discharges electrical sparks to the workpiece, eroding the unwanted material. The dielectric fluid, typically deionized water, cools and flushes away debris during the process.
Due to its ability to produce fine detailed cuts with tight tolerances, it’s especially popular for manufacturing dies, punches, and tools, as well as for parts requiring complex shapes or delicate geometries without inducing mechanical stresses.
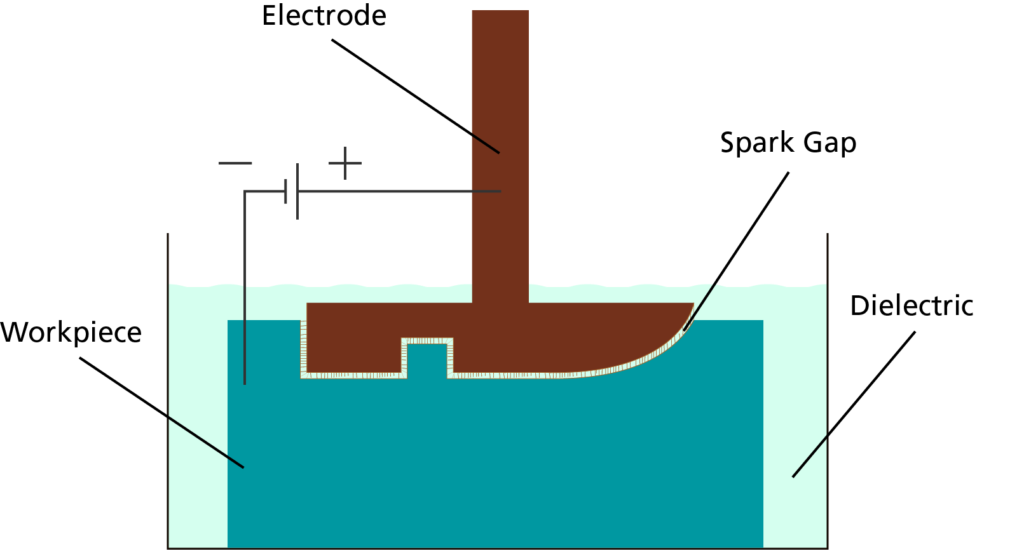
Sink EDM (Ram/Die Sinker EDM)
Sink EDM, often used for mold-making or tool and die industries, involves an electrode which is carefully machined to mirror the desired shape on the workpiece. This electrode, often made of graphite or copper, descends into the workpiece, discharging electrical sparks across the gap.
Both the electrode and the workpiece are submerged in dielectric fluid, usually oil or deionized water, which helps control the sparking process. Material is eroded from the workpiece to form the desired shape.
Advanced control systems maintain consistent sparking and provide excellent surface finishes, making it ideal for producing complex cavities, sharp corners, and detailed geometries.
Hole-Drilling EDM
Hole-Drilling EDM is engineered to create deep, precise, and small-diameter holes. The process employs a tubular electrode that rotates and discharges electrical sparks to the workpiece.
High-pressure dielectric fluid, typically oil, is injected through the electrode to flush out eroded material, ensuring clean and accurate hole production. The depth-to-diameter ratio can be quite high, allowing for extremely deep holes relative to their diameter.
This technique is invaluable for producing starter holes for Wire EDM operations or crafting cooling holes in components like gas turbine blades in aerospace applications. The precision and repeatability of this process are commendable, especially for challenging materials and critical applications.
Advantages of Wire EDM Machining
Wire EDM offers high precision and low cutting force for hardened conductive materials, making it useful for complex shapes, narrow features, and controlled surface finishes.
Transform Your Ideas into High-Quality Components with Our Wire EDM Machining Services
Get instant quoteWire EDM Machining Compatible Materials
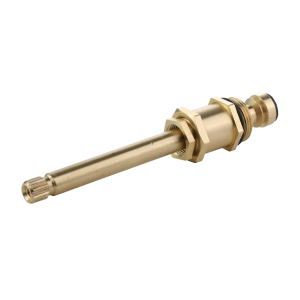
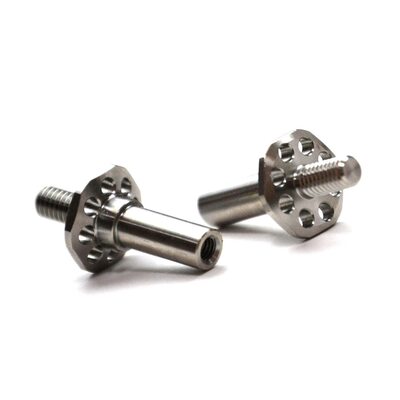
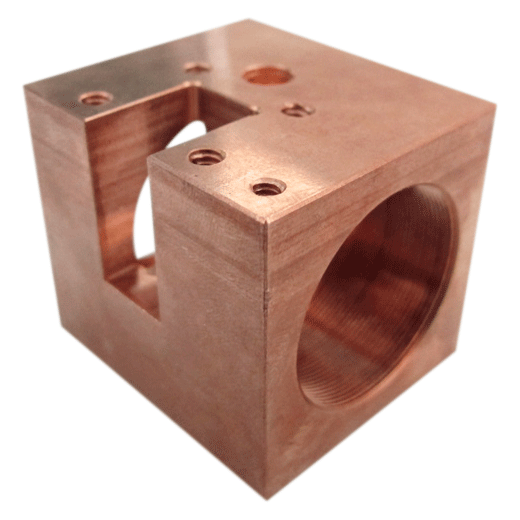
Whether you need hardened steel, aluminum, titanium, copper, or another conductive metal, YXT can review the material and geometry for your wire EDM project.
Wire EDM Machining Application
Explore common industries and applications for wire EDM machining.
Aerospace Components
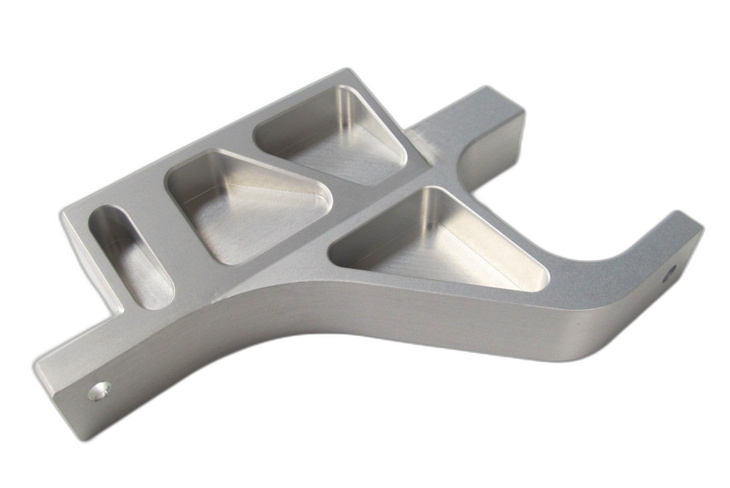
Produce complex profiles and tight features for aerospace tooling, engine systems, and structural components.
Medical Devices
Create intricate conductive components for instruments, fixtures, and device-development applications.
Automotive Components
Support precision fuel-system, drivetrain, tooling, and development components for mobility projects.
Gears and Splines
Machine accurate profiles for gears, splines, and transmission components where conventional tooling has limited access.
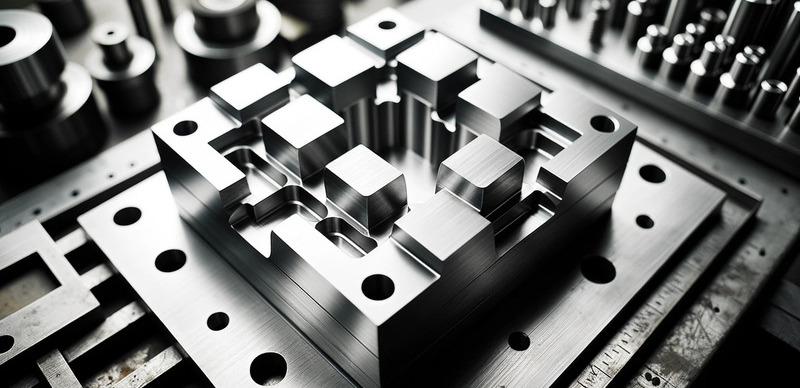
Tool and Die Making
Produce precise molds, dies, inserts, and tooling features used in repeat manufacturing.
Prototyping
Develop precision prototypes for design verification and testing before full-scale production.
Why Choose Us For Wire EDM Machining Services
Cost-Efficient Planning
YXT reviews geometry, material, wire path, and setup strategy to control machining time and avoid unnecessary project cost.
Precision Tolerance Review
Critical dimensions are reviewed against feature size, material, wire diameter, surface finish, and inspection method before production.
Reliable Delivery
Production schedules are planned around material availability, programming, machining, and inspection requirements, with urgent needs reviewed case by case.
Responsive Engineering Support
Drawing questions, material concerns, and process changes are reviewed early so the project can move forward with fewer surprises.
Wire EDM Machining Services FAQ
What materials can you cut with wire EDM?
Wire EDM can cut any electrically conductive material, including hardened steel, titanium, nickel alloys, and carbide.
How accurate is wire EDM?
The tolerance of wire EDM is usually around ±0.001 inches (+/- 0.025 mm), with even higher accuracy possible for skilled operators.
What size parts can you make with wire EDM?
Wire EDM has no size restrictions, as long as the part can fit submerged in the work tank. Micro-wires enable cutting of parts with fine details.
What surface finish does wire EDM produce?
The surface will be uniform but slightly rough. Finish is typically around 12-25 microinches Ra, suitable for many applications without extra polishing.
How do you prevent wire breakage?
YXT use reliable wire threading systems, optimized cut settings, and preventative maintenance to maximize wire life and minimize untimely breakage during machining.
How do you inspect finished parts?
We thoroughly inspect all critical dimensions and compare to your specifications using advanced measurement equipment like CMMs and optical comparators. Statistical process control ensures consistent quality.