
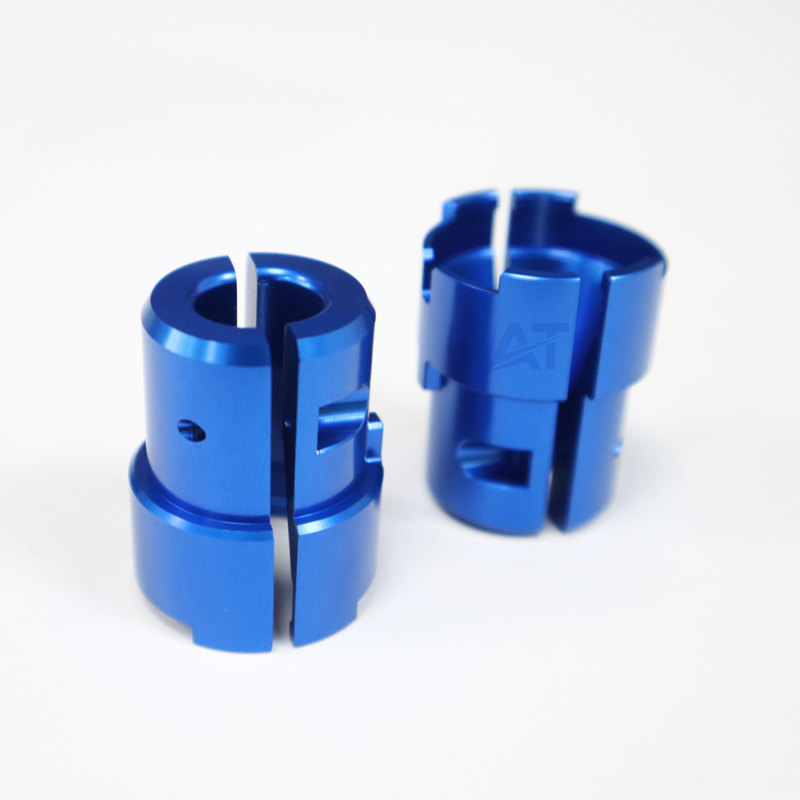
Aluminum CNC mask anodize for grounding is a drawing task: keep anodic oxide off the earth path. Type II (1.8-25.4 µm) and Type III (12.7-114 µm) films are electrical insulators. Hatch every grounding pad, chassis stud, EMI finger land, and connector shell seat on the PDF. Give a pad size a shop can tape or fixture (often 6-10 mm, smaller with plugs or custom masks). Put rack marks on a different face. If the bare aluminum also needs corrosion resistance, add a conversion-coating note on the masked areas only. Pair STEP + PDF with alloy (6061-T6 is the usual housing), Type, Class, thickness, and a continuity check. If you anodize all over, the housing will look finished and will not earth.
US and EU electrical and mechanical engineers often split the job: the PDF says “black anodize,” the schematic says “chassis ground on the standoff.” A Dongguan mill will coat the standoff unless you hatch it.
Use the same finish language as anodizing finishing services and the alloy notes on aluminum CNC machining.
Key takeaways
- Anodize is insulation. Grounding requires a mask, a later mill, or a fastener that cuts oxide (the last is a poor drawing strategy).
- Pads belong on bosses, not on 0.6 mm membranes. Size them 6-10 mm when you can.
- Rack contact is not a grounding spec. Assign both zones.
- Inspect continuity after finish, not only color.
Why aluminum CNC mask anodize for grounding exists
Why aluminum CNC mask anodize for grounding exists is simple physics: the oxide grown in a Type II or Type III bath does not carry chassis current. MIL-A-8625 Type II and Type III are corrosion and wear coatings. They are not contact platings.
MIL-A-8625F (issued 2003, validation notice 2019) puts Type II at 1.8-25.4 µm (0.00007-0.0010 in) and Type III at 12.7-114 µm (0.0005-0.0045 in), with 0.002 in (50.8 µm) as the Type III nominal if thickness is blank. Every one of those films is an insulator. A 12 µm Type II Class 2 black looks like metal and measures open circuit. A 50 µm Type III coat is simply a thicker open circuit.
If a 6061 enclosure must earth a board, gland, or EMI gasket, those lands stay bare (or conversion coated). Everything else can be Class 2 black. Do not plan to scratch a corner at incoming.
In 2024 alloy tables from the Aluminum Association, typical 6061-T6 tensile strength is about 45 ksi (310 MPa). That value does not make anodize conductive. 7075-T6 is stronger and still insulates once coated. Name the alloy so dye and mask chemistry match the stock.
Where to mask: pads, holes, bosses, and EMI lands
Put the conductive window where a fixture can reach and a screw can clamp.
Good locations: a raised boss around an M3 or M4, an EMI gasket land, a connector cutout face. Many tape masks hold at 6-8 mm. A 6-10 mm land is the drawing default. Bad locations: the middle of a 0.8 mm wall, and the only face you also marked as rack-OK.
If masked aluminum sits in a humid cabinet, add conversion coating on those pads as a second note. Conversion films typically stay usable for chassis earth. Type II / Type III do not.
ASME Y14.5-2018 (reaffirmed 2024) is how you bound the pad if size and position are functional. A floating 5 mm island with no datum will still get taped, then fail EMI because it missed the gasket.
Wall thickness around the pad matters. A 3 mm boss under an 8 mm pad is tape-friendly. A 6 mm pad in the center of a 0.6 mm lid wrinkles. Keep most housing walls at 1.0-1.5 mm and put earth on a local boss. Thin-wall machining and mask tape fight each other.
| Factor | Mask (no anodize) | Coat all over | Best for | Watch-out |
|---|---|---|---|---|
| Electrical path | Bare or conversion pad | Oxide insulates | Chassis earth, EMI lands | Anodize-all-over plus a schematic that needs earth |
| Pad size | 6-10 mm tape, smaller with plugs | Not applicable | Bosses, connector seats | Sub-3 mm islands on an A-side |
| Rack marks | Separate C-face | Shop picks a clip | Hidden boss | Rack on the only ground pad |
| Pad corrosion | Optional conversion coat | Anodic film | Indoor vs wet boxes | Raw mill finish in humidity |
| Wall under pad | Boss ≥2-3 mm | Any coated skin | Housings | Tape on 0.6 mm membrane |
Bottom line: hatch the earth path, assign a different rack face, and inspect continuity after dye. Do not plan to scratch a corner at incoming.
How to mark the drawing so the racking tech is not guessing
Use a mask legend. Hatch or color the conductive zones in a 2D view. Label: “MASK, NO ANODIZE, GROUNDING.” Point to a detail if the pad is small. State the allowed edge (a 0.5-1 mm halo of mixed film is common unless you fixture-mask).
Write the global finish separately: MIL-A-8625 Type II Class 2 black, 8-20 µm, sealed, bead blast, except masked areas. Or Type III Class 1, 25-50 µm, if wear wins. The mask note is yours. Type III at the 50.8 µm nominal is not “more grounded.” It is more insulating.
Rack marks: pick a hidden boss, a pocket floor, or the underside of a flange. Note “ELECTRICAL CONTACT / RACK OK.” Give the clip a usable area, often ≥8 mm. If you leave this blank, the shop will clip wherever current is convenient, sometimes on your earth pad, sometimes on the A-side.
Cosmetic rule: A-side coated, pads inside, rack on a C-face. If the whole exterior is cosmetic, add an internal rack boss and do not delete it in the CAD “cleanup.”
Threads that are the earth path: mask or tap after. Threads that are only fasteners into a coated boss: follow the Type II / Type III thread rule (mask M3-M5 for Type III, mask M3 for Type II if they must gauge). Do not assume a screw will cut through oxide and make a reliable earth. That is a field failure, not a spec.
For mill-and-finish as one route, keep the same language as custom CNC machining services. CNC milling of a 0.2 mm facing after anodize is salvage. Design the mask so you do not need that facing.
Procedure: aluminum CNC mask anodize for grounding
Each step names the tool and the done check.
- Identify every earth path on the schematic and the 3D. Tool: a marked-up PDF or a layer in CAD. Done when every standoff, gland, gasket land, and connector seat is either coated or listed as conductive.
- Convert each conductive feature into a maskable pad. Tool: a boss or land ≥6 mm when possible (6-10 mm preferred), or a pluggable hole. Done when a racking tech can tape, cap, or fixture it without covering a cosmetic face or collapsing a wall under 1.0 mm.
- Write two finish notes. Tool: title-block anodize spec (Type II 1.8-25.4 µm or Type III 12.7-114 µm, Class, thickness) plus a mask legend. Done when Type, Class, thickness, and “NO ANODIZE” zones are both present.
- Separate rack from ground. Tool: a hatched rack-OK face that is not a pad, clip area ≥8 mm. Done when current has a legal clip point.
- Add corrosion on pads if needed. Tool: conversion-coating callout on masked aluminum only. Done when earth pads are not left as raw mill finish in a wet environment unless you accept that.
- Program inspection. Tool: a simple continuity or milliohm check from pad to pad after finish, plus a visual of mask edge. Done when first article records a pass, not only a color photo.
- Pack the RFQ. Tool: STEP + PDF, alloy, quantity, sample if Class 2. Done when mill and anodize can be quoted as one route.
Common failure: the model shows a shiny boss and the PDF says “anodize all over.” The bath follows the PDF.
Pad sizes, plugs, and wall thickness under the mask
Pad size is a racking constraint, not a preference. Tape masks are the default on 6-10 mm bosses. Many shops hold 6-8 mm without a custom fixture. Below about 5 mm, tape lift and Class 2 dye bleed rise fast. Plugs work on holes: an M3 or M4 thread that must stay metal gets a cap, not a square of tape on the A-side. Connector seats and EMI lands often need a fixture mask so the halo stays inside 0.5-1 mm.
Wall under the pad should be a boss. 2-3 mm of aluminum under an 8 mm land takes tape pressure. A 0.8 mm membrane does not. If the housing is already in thin-wall territory (1.0 mm field, 0.8 mm windows), add a local boss for earth rather than thinning the pad into the skin. Type II at 8-20 µm on a 1.5 mm wall is a normal bath. Type III at 25-50 µm (or 50.8 µm if thickness is blank) on a 0.8 mm wall next to a taped pad is two risks stacked: oil-canning and a wrinkled mask.
If several pads sit on one face, keep at least a few millimeters of coated skin between them so tape pieces do not overlap into a messy halo. Do not put a 4 mm pad between two M3 holes and expect both threads and the pad to stay clean. Grow the boss, or tap after coating, or drop one requirement.
Write the pad on the PDF as a size, not as “grounding area.” Ø8 mm or 8 × 10 mm is quotable. “Sufficient contact” is not.
Type II versus Type III does not change the pad size rule. Type III film is thicker (often 25-50 µm, 50.8 µm if blank), so a leaking tape edge leaves a wider insulating halo. Fixture-mask Type III pads when the land is under 8 mm. Type II at 8-20 µm is more forgiving of tape, which is why 6-8 mm pads are routine on sealed black 6061 housings. On 7075 Type III rails, keep earth on a separate boss so the wear coat and the mask do not fight.
If the connector cutout is both a mechanical seat and an earth, mask the full seat, not a 3 mm stripe. A 3 mm stripe disappears under a 1 mm halo. Give the finisher a land they can see on the rack.
Inspection, dye bleed, and a worked RFQ example
Continuity is the grounding inspection. Color is the cosmetic inspection. Do both. Name a method on the PDF. A hand multimeter from pad to pad is enough for many chassis. If EMI needs a milliohm limit, write the limit and the probe points.
Dye bleed: Class 2 black can creep under tape. Fixture masks and plugs beat cheap tape on small pads. If a halo is allowed, say the width (0.5-1 mm is a common allowance). If the EMI gasket needs a clean 8 mm land, do not allow a 2 mm halo that shrinks the metal to 4 mm.
Rework: facing a coated pad after anodize is salvage, not DFM. Fix the drawing so the next lot is masked. Stripping Type III to recover a forgotten pad is slower than a hatch on the PDF.
Worked RFQ example: 6061-T6 enclosure, 150 × 95 × 35 mm, 1.5 mm walls, Type II Class 2 black 8-20 µm sealed, bead blast. Earth paths: USB connector seat 8 × 12 mm, two M3 standoff bosses with Ø8 mm pad on the top face, EMI gasket land 6 mm wide around the lid opening. Mask all of those. Plug all remaining M3. Rack-OK: underside of a 10 mm internal boss, not a ground pad. Conversion coat on masked pads. Continuity: USB seat to both standoff pads, 2-wire milliohm, record on first article. Quantity 40.
That is aluminum CNC mask anodize for grounding as a complete note. The wrong pack is “anodize black, make sure it grounds.”
Second worked example, Type III wear plus earth: 7075-T6 plate 180 × 80 × 8 mm, Type III Class 1 25-50 µm unsealed on the rail, two Ø8 mm earth pads on 3 mm bosses, H7 pivot masked, rack-OK opposite the pads. Continuity pad to pad after coating. Do not dye this 7075 part to match a 6061 Type II housing in the same assembly. Two alloys, two baths, two coupons.
When the drawing is complete, send it through YXT CNC contact. Small-batch CNC machining is the right frame while you still move pad locations between spins.
| Pad type | Target size | Mask method | Best for | Watch-out |
|---|---|---|---|---|
| Boss face | 6-10 mm | Tape or fixture | Standoff earth | Pad = rack clip |
| Connector seat | ≥8 mm land | Fixture or tape | USB, D-sub | Dye in the cutout |
| EMI gasket | 6 mm min width | Fixture | Lid lands | Halo eats width |
| Thread as earth | Plug + tap after | Plug | Studs | Oxide in the minor |
| Thin-wall island | Avoid | N/A | Do not | 0.6 mm tape wrinkle |
Bottom line: design pads to a mask method you can repeat, then inspect continuity on first article.
FAQ
Does aluminum CNC mask anodize for grounding apply to Type III too?
Yes. Type III is a thicker insulator. Mask the same pads. Type III at 12.7-114 µm (50.8 µm if thickness is blank) does not conduct because it is hard. Hatch 6-10 mm pads, keep rack marks elsewhere, and check continuity. Wear faces can be Type III Class 1 while earth pads stay masked. Do not leave a Type III film on an EMI land and hope a gasket bites through.
Can I use a rack mark as the ground point?
Most drawings should not. Rack marks vary in size and location. A hatched pad does not. The clip is an electrical contact for the bath, not a chassis earth you can probe on every unit. If a lot clips on a hidden boss, that boss is scarred, not dimensioned as a pad. Assign both zones. If you only have one small island, grow a second boss.
How large should a grounding pad be?
6-10 mm is easy to mask. Many shops hold 6-8 mm with tape. Smaller is possible with plugs or fixtures. Write the size. Sub-3 mm islands on an A-side fail by tape lift and Class 2 dye bleed. Put the pad on a boss with enough wall (2-3 mm) so tape pressure does not oil-can a 0.8 mm skin. State the allowed halo.
Do threaded holes need masking for earth?
If the thread is the earth path, mask or tap after. If the boss face is the earth, mask the face. A screw through coated threads is not a reliable earth. Type II 8-20 µm in an M3 minor diameter can still insulate. Type III at 25-50 µm will. Write which surface is conductive. Plug the hole if the thread must stay metal.
Will conversion coating on the pad kill conductivity?
Typical conversion films stay usable for chassis earth. Anodic oxide does not. Use conversion on masked aluminum when humidity or fingerprints matter. Keep that note separate from MIL-A-8625 Type II / Type III. Do not call conversion “light anodize.” If EMI needs a milliohm limit, prove it on a conversion-coated coupon of the same 6061 lot. Raw mill finish on a pad is fine indoors if you accept fingerprints and oxidation over time.
Where should rack marks go relative to ground pads?
On a different face. Use a hidden boss, pocket floor, or flange underside with a clip area ≥8 mm. Never share a 4-6 mm island between rack and earth. A-side cosmetics should not take the clip. If the exterior is fully cosmetic, add an internal rack boss and keep it on the STEP. The bath needs current. Give it a legal place.
Can I mill the pad after anodize instead of masking?
You can, as salvage or as a planned secondary. Masking is cleaner and cheaper on a housing that already has bosses. A post-anodize face cut through Type II or Type III leaves a bright ring and a sharp coat edge that can chip. If you plan the mill, call the remaining pad size (still 6-10 mm if you can) and inspect continuity. For new drawings, hatch the mask.
Call out aluminum CNC mask anodize for grounding as hatched pads (6-10 mm when you can), a separate rack zone, and a continuity check on the PDF. Then send STEP + PDF to YXT CNC with Type II or Type III, Class, and thickness. The oxide should protect the box. It should not open the earth path.


