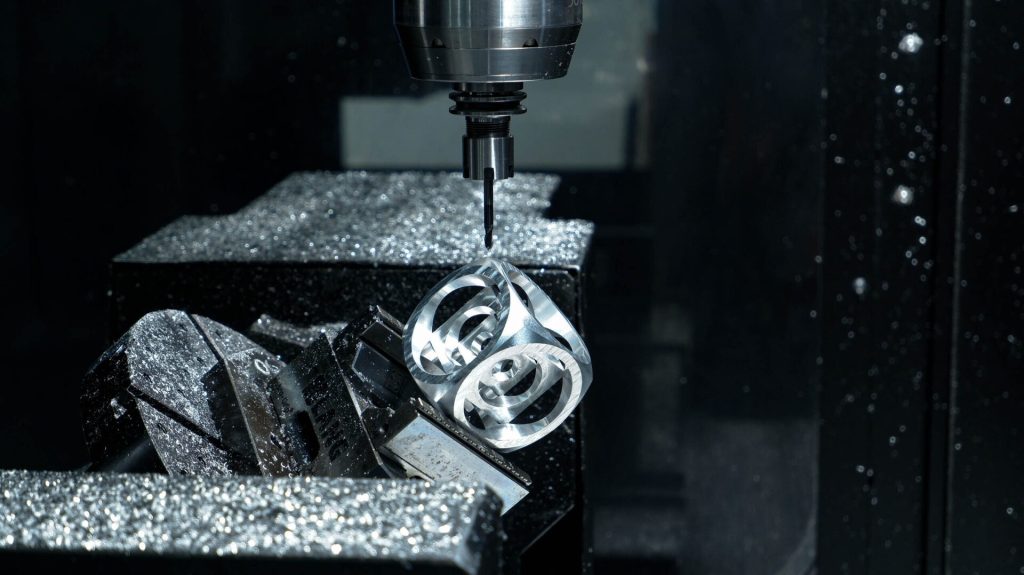
5-axis vs 3-axis CNC machining is a setup and access decision, not a quality slogan. Use 5-axis (or indexed 3+2) when the part has compound holes, undercuts, or datums that must stay in one fixture, such as a multi-face 6061 housing. Keep 3-axis for prismatic plates, 2.5D pockets, and simple brackets where a vise and a couple of flips are enough. ISO 2768-1 (1989) still governs unmarked sizes either way. ASME Y14.5-2018 datums tell you whether a third setup would break a true position you will actually inspect. Specify 5-axis when that extra setup would cost more in datum stack and fixtures than the higher machine rate.
This comparison is for a US or EU engineer choosing a process note before an RFQ to a China factory. You are not choosing a brand of machine. You are choosing how many times the part is taken out of a fixture.
If the drawing is a plate with pockets, CNC milling on 3-axis is the default. If the drawing is a housing with compound ports, 5-axis CNC machining services are justified when one setup protects the datums you will CMM.
Key takeaways
- Default to 3-axis. Move to 5-axis when you would otherwise cut a true-position chain across three or more fixtures.
- Indexed 3+2 is enough for most prismatic multi-face parts. Continuous 5-axis is for blended surfaces and changing tool tilt while cutting.
- Machine rate is higher on 5-axis. Total cost can still drop if you delete fixtures, flips, and datum restacks.
- Unmarked sizes stay on ISO 2768-1 (1989) regardless of axis count. Axes do not replace a tolerance scheme.
- Write “3+2 indexed OK” when the rotary axes only need to lock. That note stops a simultaneous program you will not inspect as a blend.
5-axis vs 3-axis CNC machining: start with this table
5-axis vs 3-axis CNC machining should be decided from setups, access, and inspection, then from hourly rate.
| Factor | 3-axis | 5-axis (including 3+2) | Best for | Watch-out |
|---|---|---|---|---|
| Setups | One orientation per clamp | Many faces in one fixture | 5-axis when 3+ flips stack datum error | Probe and fixture time still exist |
| Tool access | Vertical (or horizontal) only | Tilt and rotate | Compound holes, undercuts, deep walls | Collisions if holder and stock are not modeled |
| Typical parts | Plates, 2.5D pockets, simple brackets | Multi-face housings, angled ports | 3-axis for prismatic work | 5-axis does not fix a bad tolerance block |
| Finish on walls | Limited by tool stick-out after flips | Better tool tilt on steep walls | 5-axis for blended or steep surfaces | Stepover and tool still set Ra |
| Quote driver | Lower machine rate, more fixtures | Higher rate, fewer fixtures | 3-axis when fixtures are cheap | One-off CAM prove-out can erase the saving |
| Inspection | Re-establish datums after each flip | Probe once if the fixture holds A-B-C | 5-axis when CMM frame matches the clamp | A bad 5-axis fixture still dumps the frame |
Bottom line: keep 3-axis unless compound access or a one-setup datum scheme is doing real work on the drawing.
Count setups the way a programmer does. A plate with pockets on one face and holes on the back is two 3-axis ops: a vise, a flip, maybe dowel pins. That is normal. A housing with features on five faces plus two 30° ports is six 3-axis attitudes or one 3+2 fixture. The second path is where 5-axis earns the rate.
ASME Y14.5-2018 is the language of that choice. If true position ties holes on faces a 3-axis vise cannot see without unclamping, you are paying for rotary axes or for a complex fixture. If every inspected hole sits on one face, you are not.
When 5-axis is justified
5-axis is justified when a 3-axis process would need extra fixtures you cannot control, or tool angles you cannot reach.
Examples that usually qualify: a housing with ports that are not square to the primary datum, a part with features on five or six faces that share one true-position frame, a cavity whose walls need a shorter tool via tilt, and a blend where the tool must change orientation while cutting. Indexed 3+2 covers the first three if the rotary axes can lock. Continuous 5-axis is for the blend.
A 30° and a 45° port that must land on the same datum frame as a face seal is the textbook case. A sine plate can cut one angle. Two angles plus a seal, all to one CMM report, is where 3+2 or full 5-axis stops being a luxury. Deep walls favor tilt so the tool is 3× diameter instead of 8×. Deflection drops roughly with the cube of stick-out in simple beam terms. That is why a tilted 8 mm mill can hold size and Ra better than a long 4 mm mill on 3-axis, even if the spindle is the same quality.
Do not specify 5-axis because the part “looks complex” in a render. A ribbed plate is still 3-axis work. Bosses, pockets, and a logo do not need rotary axes. If you need sculpted continuous surfaces, ask the shop whether they support simultaneous 5-axis on that geometry. Do not assume every 5-axis mill on a website is programmed for impeller-style motion on your housing.
Custom CNC machining services will still quote 3-axis if the drawing allows it. Your job is to say when it is not allowed. “5-axis required to hold datums A-B-C in one setup” is a process requirement. “Please use 5-axis” is a preference, and preferences get dropped when the shop is busy on 3-axis vises.
When a 3-axis process should stay
A 3-axis process should stay when the part is prismatic, the flips are few, and the datums can be re-established with pins or a vise jaw.
Plates, lids, brackets, heat-sink blanks, and 2.5D pockets are 3-axis. A second op on the back face is normal. A tombstone or a simple fixture plate is cheaper than 5-axis time when the batch is large and the geometry repeats. At 200 pieces, a 3-axis fixture you will keep often beats a 5-axis program you will prove out once per revision.
ISO 2768-m per ISO 2768-1 (1989) is enough for most unmarked sizes on these parts. Medium class on 6-30 mm is ±0.2 mm. Tight holes can still be bored on 3-axis. Tight diameters can still be turned, then milled. Axis count is not a substitute for choosing mill vs turn.
If you can machine the part in two setups with a dowel-located fixture, keep 3-axis. CAM will be simpler, and more shops can bid. Collision checking is easier. Tool libraries are the standard 3-axis set: face mill, 10 mm and 6 mm end mills, drills, taps. You are not waiting on a trunnion to be free.
A common over-specify is a 6061 box with four side holes that are square to the faces. A vise, a rotary on a 4th axis, or even two extra flips will do. That is not a 5-axis drawing. Save 5-axis for the compound hole or the one-setup datum frame. If the 4th axis is already on the mill, the shop may use it without you asking. You still do not need to require 5-axis on the RFQ.
Tall thin walls on 3-axis are a tool-length problem, not an axis-count problem. Open the pocket, thicken the wall, or allow a rest pass. Tilting helps only when the wall is steep and a shorter tool can reach. A 1.2 mm wall in a 40 mm pocket chatters on 5-axis too.
5-axis vs 3-axis CNC machining for housings and compound holes
5-axis vs 3-axis CNC machining for housings comes down to whether the port axes share a datum you will CMM.
A 6061 electrical housing with square faces and pockets is 3-axis, maybe 3+2 if you want four sides in one clamp. A manifold with 30° and 45° ports that must land on the same true position as a face seal is 5-axis or 3+2 with a probed rotary. The second part fails in 3-axis not because the mill is inaccurate, but because each flip rebuilds the datum. A 0.02 mm restack on each of three flips is enough to miss a 0.05 mm true-position frame even when each hole was “on size” in its own setup.
Deep walls favor tilt so the tool is shorter. That can improve both size and Ra. It does not automatically hold ±0.005 mm. Geometry, stick-out, and inspection still govern. Type II anodize per MIL-A-8625F (1993) still builds 5-25 µm on either process. Axes do not cancel coating.
Write “3+2 indexed OK” on the RFQ if you do not need simultaneous motion. Many housing jobs never need the rotary axes to move during the cut. The table locks at 32°, the mill cuts as 3-axis, then the table indexes to the next face. That note stops the shop from quoting a more expensive continuous program with tiny stepovers on surfaces you will never blend-inspect.
| Geometry test | 3-axis answer | 3+2 / 5-axis answer | What to write on the RFQ |
|---|---|---|---|
| 1-2 faces, 2.5D pockets | Stay 3-axis | Waste of rotary time | 3-axis acceptable |
| 4 square sides, holes 90° | 3-axis or 4th axis | Optional 3+2 for one clamp | 3-axis or indexed 4th OK |
| Two compound angles, one TP frame | Extra fixtures, datum risk | Prefer 3+2, probe the rotary | 3+2 required to hold A-B-C |
| Blend / variable tilt while cutting | Cannot do honestly | Continuous 5-axis | Simultaneous 5-axis required |
| Batch 200, existing 3-axis fixture | Keep the fixture | Only if you scrap the fixture | Keep 3-axis unless datums fail |
| Tool > 5×D in a tight pocket | Open pocket or accept chatter | Tilt to shorten the tool | 3+2 allowed for tool tilt |
Bottom line of this table: square prismatic work stays 3-axis. Compound datums and tool tilt move you to 3+2. Only blends need simultaneous motion.
Decision tree you can put on the RFQ
Use this tree. Do not end in “see how you feel.”
- Count setups a 3-axis mill would need to reach every machined face. If the answer is 1 or 2, specify 3-axis.
- Check the ASME Y14.5 datum frame. If critical holes live on faces those 1-2 setups cannot see, specify 5-axis or 3+2.
- Check tool length. If a 3-axis path needs an end mill longer than about 5× diameter in a tight pocket, prefer tilt (5-axis/3+2) or open the pocket.
- Check surfaces. If a wall must be blended while the tool tilts, specify continuous 5-axis. If not, indexed is enough.
- Check batch and fixtures. If you already own a 3-axis fixture for 500 pieces, keep 3-axis even if 5-axis could do it in one clamp.
Put the result as a process note: “3-axis acceptable” or “5-axis or 3+2 required to hold datums A-B-C in one setup.” Write the CMM features on the drawing. Axis count without an inspection list is a preference, not a requirement.
Send the STEP and datum scheme through YXT CNC contact. Ask which axis count they would program, not whether they “have 5-axis.” A shop can own a 5-axis mill and still quote your plate on a vise. That is the correct answer when the plate does not need rotary axes.
Worked RFQ: plate stays 3-axis, housing goes 3+2
Two parts, same buyer, same 6061-T6, same qty 10 / 50. The process note should not be the same.
Part P-41001 cover plate, 180 × 120 × 10 mm. Pockets 6 mm deep, 8× M4 on the top face, 4× Ø5.5 through on the same face, datum A the bottom. 3-axis count: two setups (top and a light back-face clean-up). No compound angles. Tool stick-out under 3×D. RFQ note: “3-axis acceptable. ISO 2768-m. FAI on A and the M4 pattern. Type II black 8-12 µm, dimensions before coat.” Do not write 5-axis. You will lose bidders and pay a trunnion rate for a vise job.
Part P-41002 valve housing, 90 × 70 × 55 mm. Datum A is a seal face. Two ports at 32° and 48° to A, true position 0.08 mm to A-B-C, plus holes on four square sides. 3-axis count: five or six attitudes if you chase every face with flips. Tool into the 32° port would be long without tilt. RFQ note: “5-axis or 3+2 required to hold datums A-B-C in one setup. Indexed 3+2 OK. Simultaneous not required. CMM TP on both ports and the seal. Mask the two ports for Type II.”
Header lines you can paste:
P-41001 Rev A | 6061-T6 plate | 3-axis OK | qty 10/50 | FAI hole pattern | FCA Shenzhen
P-41002 Rev A | 6061-T6 | 3+2 required for A-B-C | qty 10/50 | CMM TP on 32° and 48° ports | FCA Shenzhen
That is a 5-axis vs 3-axis CNC machining decision written so the estimator does not have to guess. The failure mode is putting both parts on one RFQ line that says “5-axis housing work” and watching the plate get the housing rate.
If P-41002 later loses the compound angles in a redesign, bump the revision and change the process note back to 3-axis. Process notes should follow the datum scheme, not the old quote.
FAQ
Is 5-axis always more accurate than 3-axis CNC machining?
No. Accuracy comes from fixture, tool, thermal control, and inspection. 5-axis helps when it removes datum transfers. A probed 3-axis bore in a stiff fixture can beat a long-tool 5-axis cut on a floppy wall. Rotary axes add their own positioning error if they are not calibrated and probed. Use 5-axis to keep A-B-C in one clamp when the drawing’s true position needs that. Do not use it as a substitute for a short tool, a rest pass, or a realistic ISO 2768 class on unmarked faces.
When is 3+2 enough instead of simultaneous 5-axis?
3+2 is enough when you lock a tilt, then cut as 3-axis. Use simultaneous 5-axis when the tool must change orientation during the cut. Most housings, manifolds, and multi-face brackets are indexed work: 32°, cut the port, index to 48°, cut the next, mill the square sides. Blends, variable-draft cavities, and some impeller-like surfaces are simultaneous. If you will inspect planes, holes, and true position, not a scallop height on a freeform wall, write “indexed 3+2 OK.” You avoid a continuous program and a finish strategy you do not need.
Does 5-axis replace tight tolerances on the drawing?
No. Unmarked sizes still follow ISO 2768-1 (1989). Call fits and datums with ASME Y14.5-2018 either way. A 5-axis mill can still leave a 0.05 mm dish on a large as-milled face. Coating still builds 5-25 µm. Thin walls still chatter. Put 5 µm or a tight true position only on features you will gauge, and name the process (3+2, grind, finish bore) that makes that band real. Axis count on the RFQ is access control. It is not a tolerance block.
Is 5-axis faster for prototype housings?
It can be when it deletes fixtures and flips. It can be slower when CAM and prove-out dominate a one-off. Qty 1 with a new simultaneous program, a collision check, and a trunnion prove-out can burn more calendar time than two 3-axis vises a programmer already trusts. Qty 10 of a 3+2 housing often wins on both time and datum control. Ask the shop which path they would actually run for your lot size. “We have 5-axis” is not a cycle-time promise.
Can 3-axis machine angled holes?
Yes, with a sine fixture or a second setup. Use 5-axis when many angles share one datum frame. One 15° hole on a bracket is a sine plate or a cheap angle block. Four compound ports plus a seal to one CMM report is not. The cost of 3-axis is not the angle. It is rebuilding datums after each unclamp. If you can live with each angle in its own frame, 3-axis stays. If incoming QA overlays all ports on A-B-C, write 3+2.
Should I require 5-axis on the RFQ for a simple bracket?
No. Require 3-axis. You will get more bidders and a process that matches the part. A simple bracket with 2.5D pockets and square holes does not use rotary axes in a useful way. Forcing 5-axis shrinks the bidder list to shops that will park your part on a trunnion and bill the rate. Put “3-axis acceptable” in the header so a vise shop does not self-reject. Save the 5-axis requirement for compound access or a one-setup datum scheme.
How many setups is too many before I switch to 5-axis?
Three or more setups that all carry inspected datums is the usual trip point. Two setups (top and back) are normal 3-axis. A third and fourth flip on a true-position chain is where restack error and fixture cost pile up. Count only setups that touch features you will CMM or gauge. Cosmetic faces that can float on ISO 2768-m do not justify a trunnion by themselves. If batch quantity is high and a dedicated 3-axis fixture already exists, you can stay on 3-axis past three ops. New work with no fixture usually should not.
Does 5-axis mean I can ignore internal corner radii?
No. A 0.2 mm internal corner still wants a 0.4 mm mill, and that mill still deflects, even when the head is tilted. Tilt can shorten stick-out. It does not invent a stiff 0.4 mm tool. Keep fillets at a real end-mill radius (R2 or R3 for many pockets). If a corner must be sharp, note EDM or a dogbone. Axis count does not replace DFM on radii or walls.
On 5-axis vs 3-axis CNC machining, keep 3-axis for prismatic plates and two-setup brackets. Specify 5-axis or 3+2 when compound access or a one-setup datum frame is what you will CMM. Send the STEP and datum scheme via YXT CNC contact and ask for the axis count they would actually program.